Paali
A tablet for the press shop floor: one tile per line, OEE that tells the truth, and the reason for a stop logged in two taps with gloves on.
A studio concept: a fictional product we designed and built to show how we work. Not a client project.
Downtime that is not written down did not happen.
Paali is a product we invented for a press shop in Chakan: Indrayani Pressworks, Plant 2, Bay C. Six lines, from an 800 tonne transfer press to a roller hem cell, making brackets, rails and control arms for car makers. Shift B runs from two in the afternoon to half past ten.
When a line stops, the reason usually goes on a paper sheet at the end of the shift, from memory. So the plant's numbers look better than the floor feels, and nobody knows which stops to fix first. Paali puts the reason on the line tile, at the moment it stops, in two taps. The PLC already knows the fault code, so the likely reason is suggested and the right team is paged as soon as it is picked.
We designed the brand and the tablet for gloves, glare and arm's length, and built it as a working prototype with a live OEE model. The plant, the people and the figures are fictional.
- 01
Show every line's state across the bay, readable from two metres away.
- 02
Turn a stopped line into the loudest thing on the screen, and only that.
- 03
Log the reason in two taps, with the PLC's best guess first.
- 04
Keep OEE honest: a stop costs points, and the number does not bounce back.
Line 3 stops at 16:41. Two taps.
The prototype's own model, rebuilt: every number comes from each line's shift timeline, and OEE is availability times performance times quality, worked out live. Time runs ten times faster here. Tap the red tile, then tap a reason.
Lines
6 lines · 4 running · 1 changeover · 1 idle
Stopped at 16:41:25 · PLC E-214 main motor overload
Why did the line stop?
Tap one reason. You can add a note later.- 0Line stops
- 1Tap the tile
- 2Tap the reason
- ✓Back up, OEE kept honest
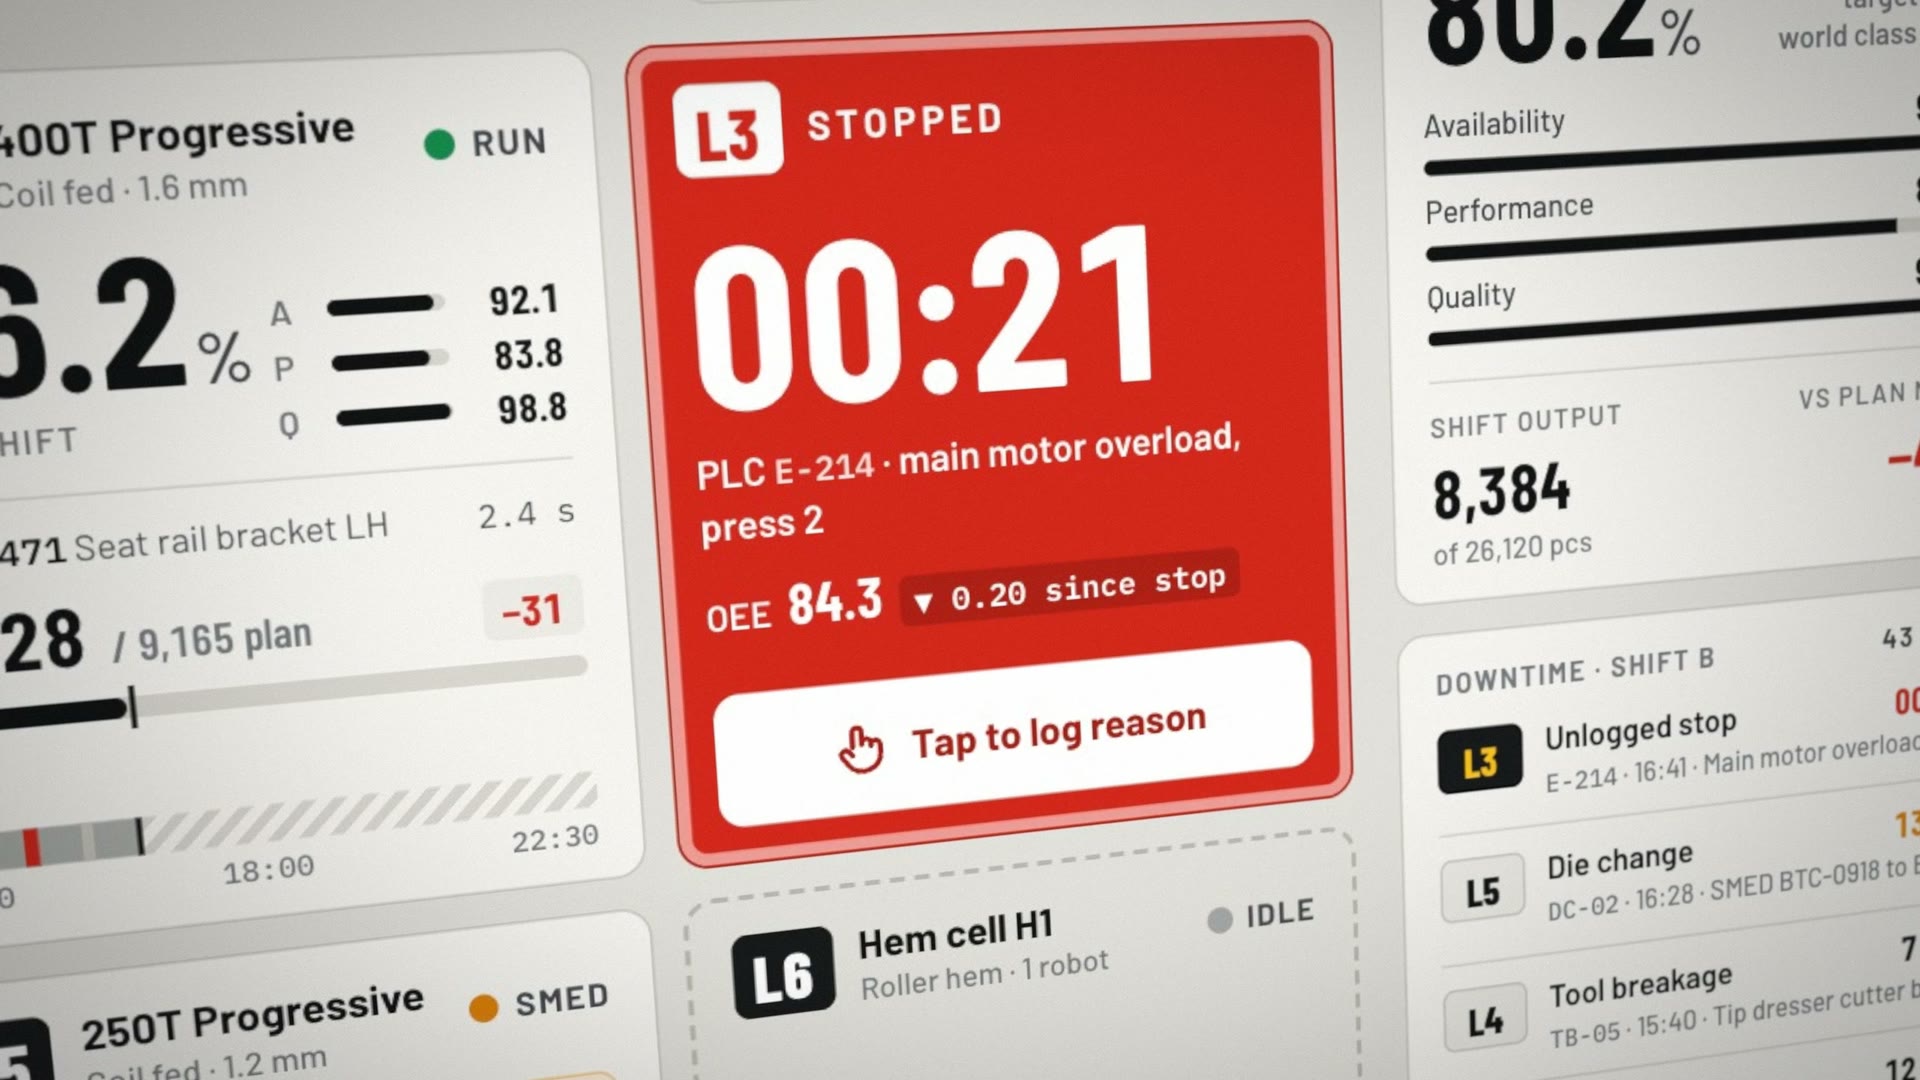
Red means stopped. Nothing else is red.
The tile turns alarm red and pulses, the timer counts up, and OEE shows what the stop has cost so far. One button: tap to log the reason.
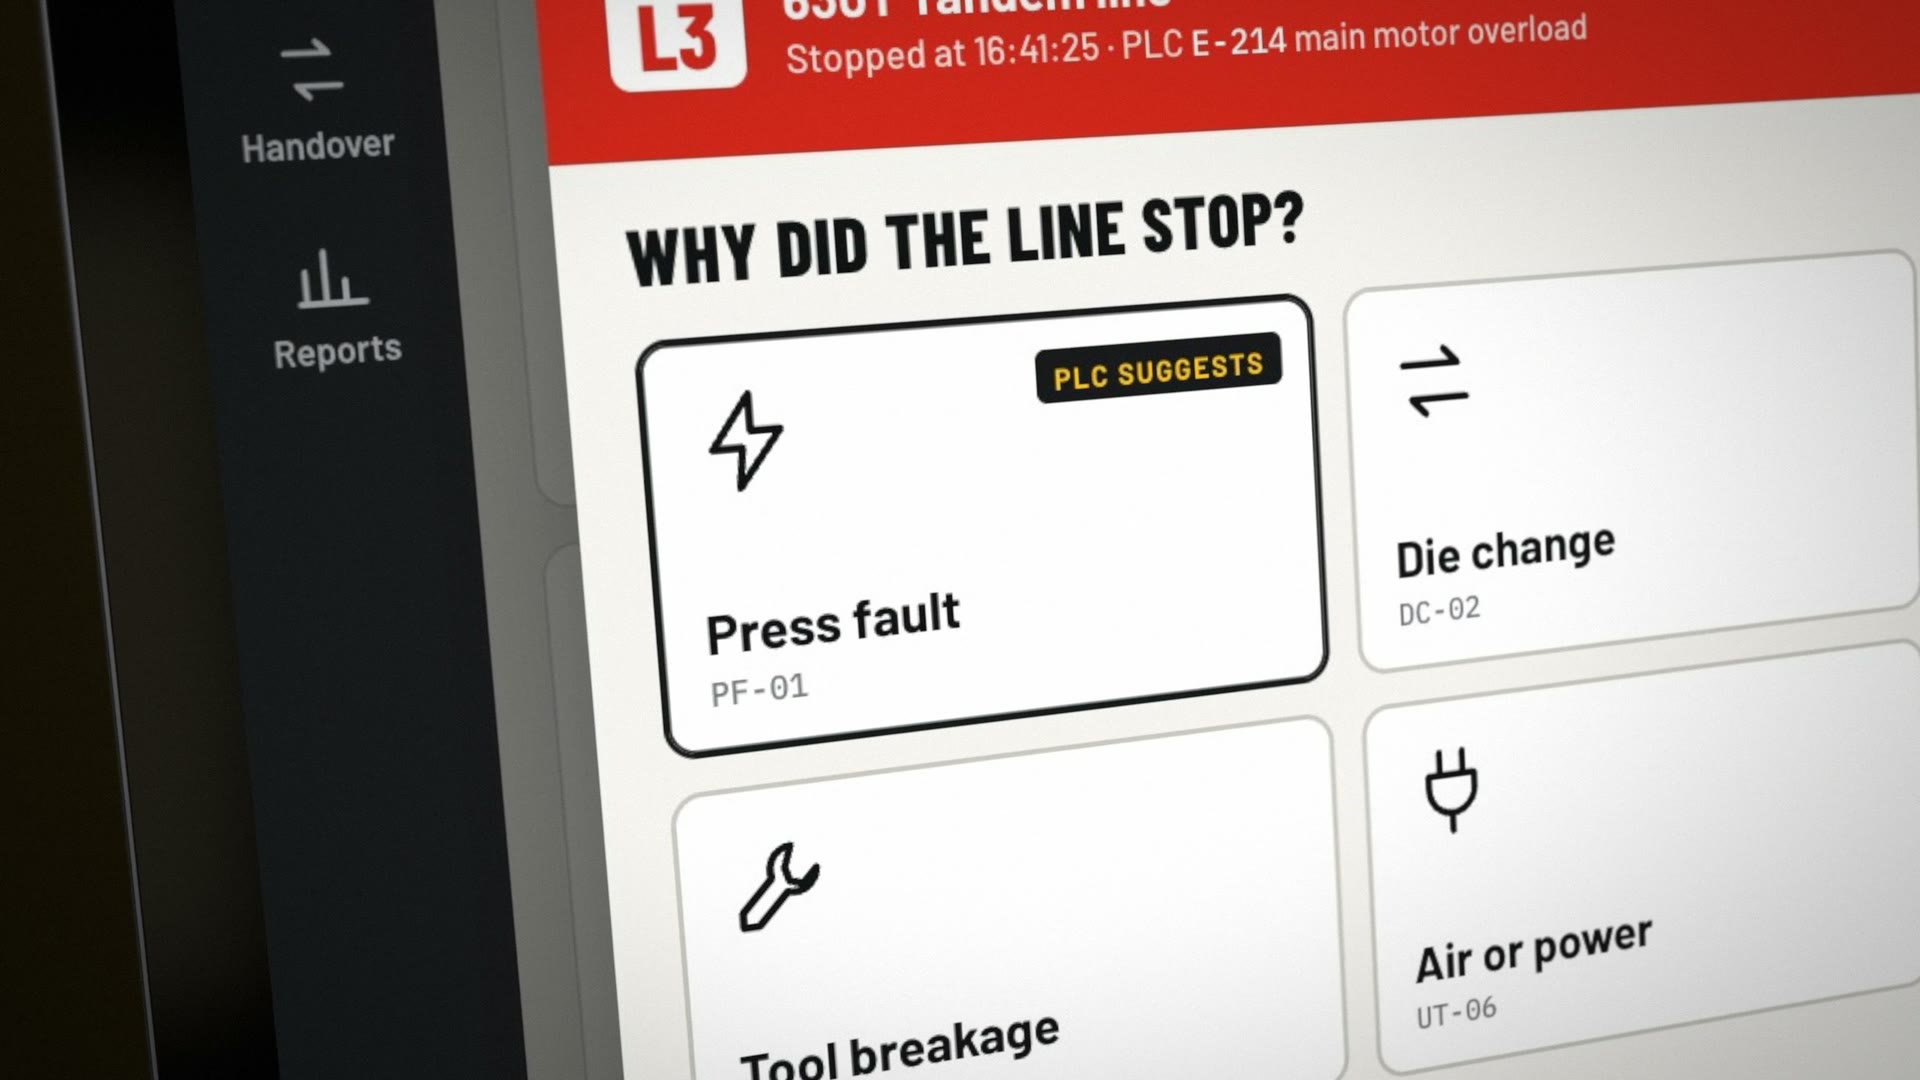
The PLC suggests, a person decides
Eight reasons in tiles big enough for a gloved finger. The fault code points at a press fault, so that one is marked. One tap logs it and pages maintenance.
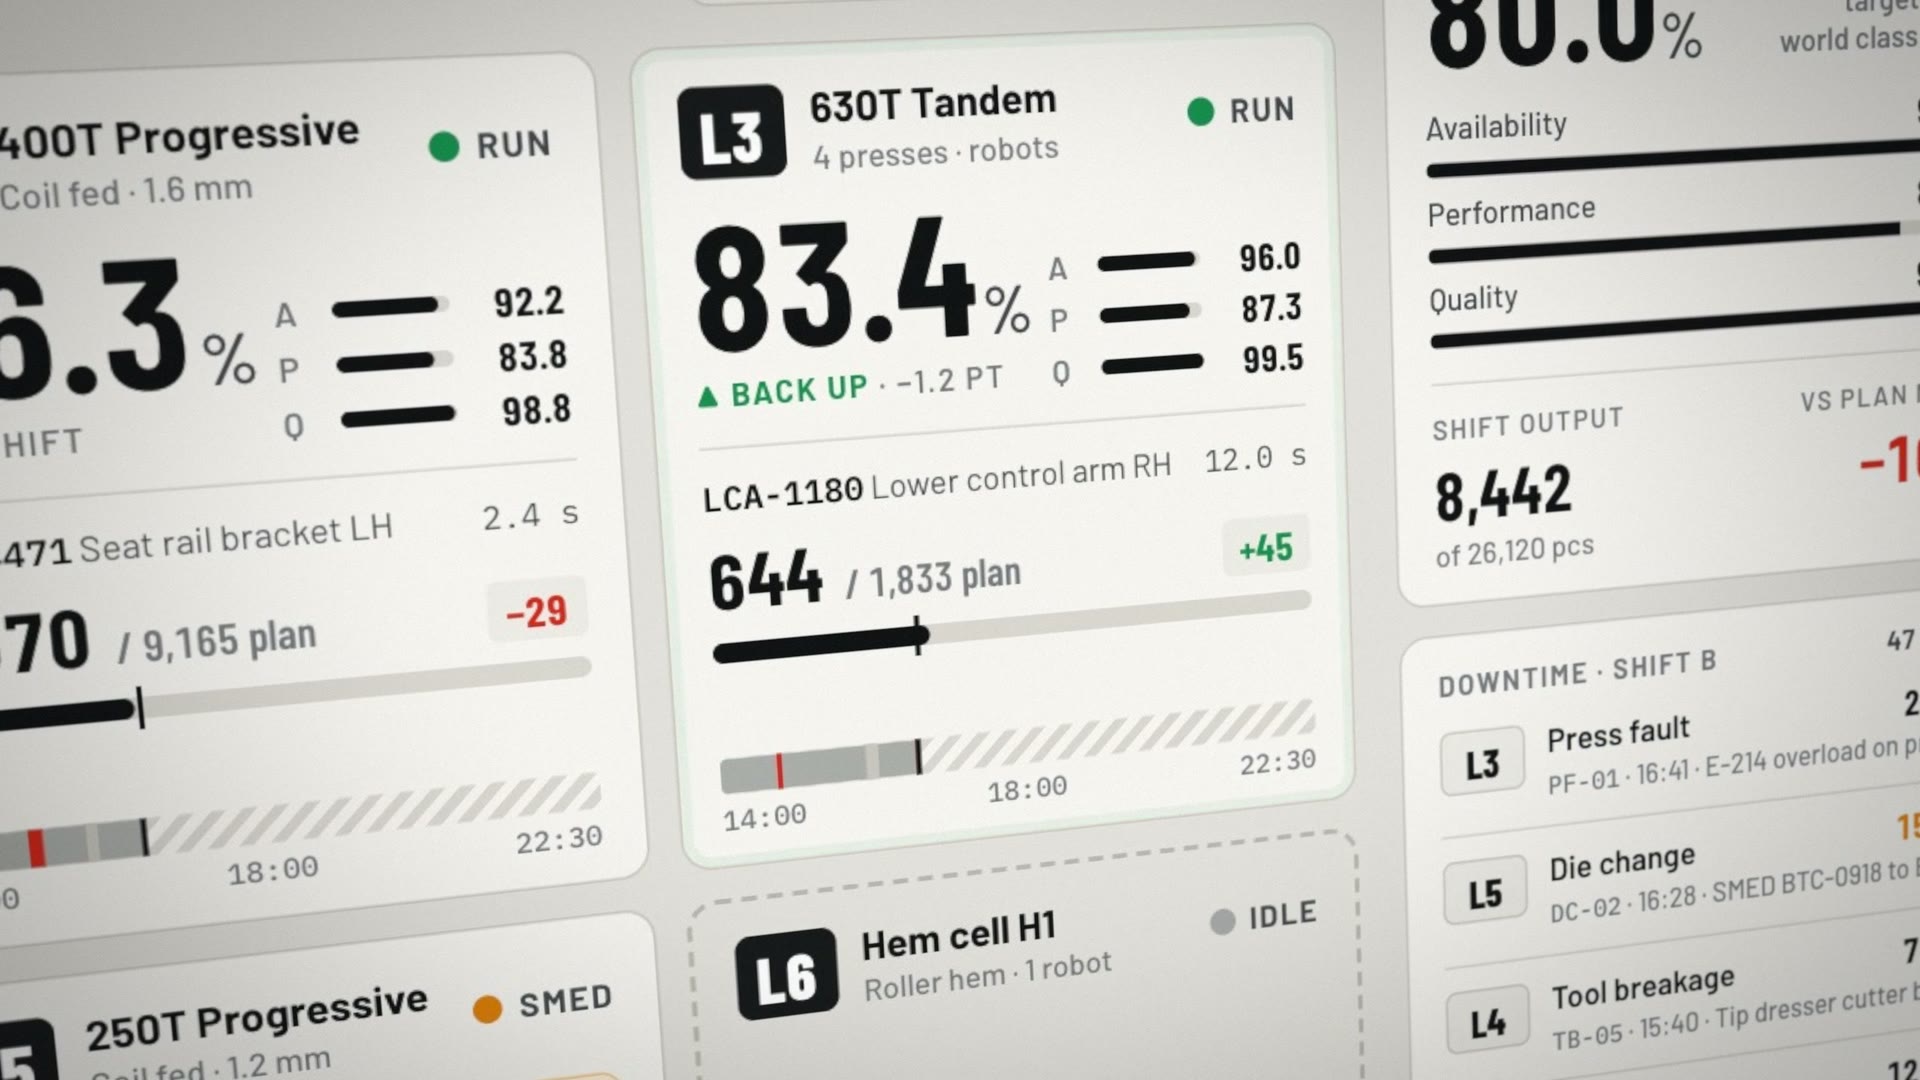
Back up, and honest about it
When the line restarts, the tile says so and shows the points the stop cost. OEE does not jump back to where it was. The stop is in the log, with who logged it.
Built for gloves, glare and arm's length.
A press shop is loud, bright and full of people holding things. The tablet is mounted on a pillar and read from across the aisle, so every decision started from the floor, not from a desk.
Targets the size of a thumb
Reason tiles are 150 pixels tall on the tablet, and the button on a stopped tile is 52. Nothing needs a fingertip.
Concrete paper, black ink
A light concrete ground and heavy condensed numerals stay legible under sodium lamps and daylight from the roof sheets.
Numbers you can read walking past
OEE in 66 pixel numerals, the stop timer in 86. State is a word and a colour, never colour alone.
Grey is normal
Running lines are grey and calm. Colour is spent only on what needs a person: red for stopped, yellow for logged and waiting, amber for a die change.
Concrete, graphite and safety yellow.
Design system#E2E0DA
#F5F4F0
#17191B
#111213
#FFC20E
#D4271B
#17914F
#DE7F0A
#3D5B78
Up next
Have something to build? We'd love to hear about it.